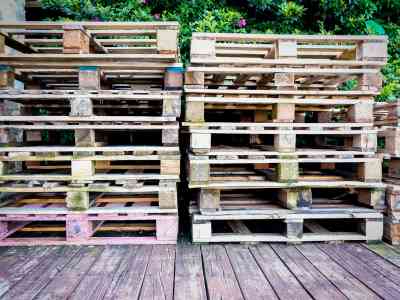
In today’s globalized business environment, efficient logistics and supply chain management are crucial. Pallets play a significant role in this domain, and choosing the right type can impact both operational efficiency and regulatory compliance. Heat-treated pallets offer several advantages, especially for businesses involved in international trade. Understanding these benefits can lead to improved sustainability, cost savings, and compliance with international standards.
Understanding Heat-Treated Pallets
Heat treatment is a process used to sanitize wooden pallets, making them suitable for international shipping. This process involves heating the pallets to a specific temperature to eliminate pests and pathogens, ensuring that they meet the International Standards for Phytosanitary Measures No. 15 (ISPM 15).
Benefits of Heat-Treated Pallets
- Compliance with International Regulations: Heat-treated pallets meet ISPM 15 standards, which are mandatory for global shipments. This compliance prevents potential delays and fines at customs checkpoints. Discover expert strategies here.
- Enhanced Durability: The heat treatment process strengthens the wood, reducing the risk of breakage during handling and transit.
- Environmental Friendliness: By using heat rather than chemical treatments, these pallets are more eco-friendly, aligning with sustainable business practices.
- Reduced Risk of Contamination: With pests and pathogens eliminated, heat-treated pallets minimize the risk of contamination, protecting goods during transport.
- Cost-Effective: While the initial investment might be higher, the long-term savings from reduced damage and compliance with international standards can be significant. Learn about our tailored solutions.
Application in Various Industries
Heat-treated pallets are versatile and beneficial across numerous industries. For manufacturers, they ensure that products reach international markets without customs issues. In the food and beverage industry, they uphold hygiene standards by reducing contamination risks. The healthcare sector benefits from the added assurance that pharmaceuticals are transported safely and securely.
Key Considerations for Implementation
Transitioning to heat-treated pallets requires thoughtful planning. Businesses should:
- Evaluate the specific needs of their industry and supply chain.
- Consider working with suppliers who offer certified heat-treated pallets. Explore advanced guides and tips.
- Assess the cost-benefit ratio, keeping long-term savings in mind.
Future-Proofing Business Operations
As global trade continues to evolve, regulations may become even more stringent. By adopting heat-treated pallets now, businesses can future-proof their operations against potential regulatory changes, ensuring continued compliance and operational efficiency. Find out more about this approach.
In conclusion, the adoption of heat-treated pallets offers a strategic advantage for businesses engaged in international trade. By ensuring compliance, enhancing durability, and promoting sustainability, these pallets not only meet current logistical needs but also prepare businesses for future challenges. Investing in heat-treated pallets is a decision that can yield significant dividends in operational efficiency and global market competitiveness.